Call: 08045813591
 Send Inquiry

 Send Inquiry
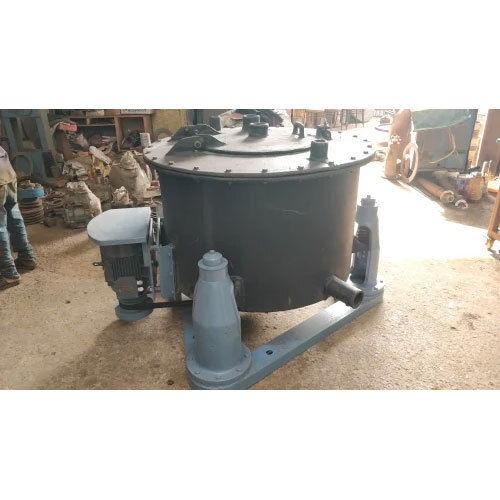
Lifting Bag Centrifuge Machine
Price 230000 INR/ Unit
MOQ : 1 Unit
Lifting Bag Centrifuge Machine Specification
- Noise Level
- Low noise operation
- Machine Type
- Lifting Bag Centrifuge
- Frequency
- 50 Hz
- Drive
- Direct / Belt Drive
- Model No
- Custom/Standard available
- Motor Power
- 2-10 HP
- Frame Type
- Heavy-duty welded frame
- Cooling System
- Not typically required (air-cooled motor options available)
- Lubricating System
- Grease/Oil Lubrication
- Control System
- PLC / Manual
- Operating Temperature
- Up to 80C
- Production Capacity
- 50-500 kg/hr
- Power Rating
- As per customer requirement, usually 3-7.5 kW
- Accuracy
- High separation efficiency
- Connectivity Options
- Panel integration, digital readouts (option)
- Features
- Lifting bag system, vibration free operation, corrosion resistance, user-friendly interface
- Voltage
- 415V AC, 3 Phase
- Product Type
- Lifting Bag Centrifuge Machine
- Technology
- Mechanical Separation
- Power Source
- Electric
- Operating Type
- Automatic / Semi-Automatic
- Power
- Varies (typically 2-10 HP depending on model)
- Pressure
- Standard Atmospheric Pressure
- Surface Treatment
- Polished Stainless Steel
- Dimension (L*W*H)
- Customizable - Standard options available upon request
- Weight (kg)
- Approx. 600-1200 kg (model dependent)
- Color
- Silver
- Usage & Applications
- Industrial
- Safety Interlocks
- Provided for operator safety
- Bearing Type
- Heavy-duty ball/roller bearings
- Working Speed
- Up to 1000-1500 RPM
- Load/Unload Method
- Lifting Bag with Hook System
- Mounting Type
- Floor Mounted
- Application Industries
- Pharmaceutical, Chemical, Food Processing, Textile, Dyestuffs, Environmental
- Basket Material
- Stainless Steel SS 304/SS 316
- Discharge Type
- Top Discharge / Bag Lifting
- Foundation Requirement
- Minimal, standard industrial base
- Finish
- Mirror / Matt finish as per requirement
- Sealing
- Mechanical Seal / Gasket Seal
- Compliance
- GMP, cGMP Standards (where applicable)
- Installation Service
- Available (Optional)
- Basket Diameter
- 450 - 1200 mm (depends on model)
Lifting Bag Centrifuge Machine Trade Information
- Minimum Order Quantity
- 1 Unit
- Supply Ability
- 4 Units Per Month
- Delivery Time
- 30 Days
Lifting Bag Centrifuge Machine About
Jump on the rare opportunity to own a top-ranking Lifting Bag Centrifuge Machine, brilliantly engineered for demanding industrial applications. Crafted with sublime precision using SS 304/SS 316 stainless steel and a heavy-duty welded frame, this machine ensures high separation efficiency and corrosion resistance. Operators benefit from a user-friendly interface, powerful safety interlocks, and minimal foundation requirements. Designed for GMP/cGMP compliance, its customizable models feature lifting bag systems and vibration-free operation. Grab yours now for an exceptional upgrade to your production line!
Exceptional Applications & Advantages
The Lifting Bag Centrifuge Machine excels in pharmaceutical, chemical, food processing, textile, dyestuffs, and environmental sectors. Its advantage lies in a unique lifting bag system that simplifies product discharge and minimizes manual handling. Site of application ranges from advanced laboratories to full-scale industrial plants, where the brilliance of this machine is evident through seamless operation, high durability, and superior separation results, making it a must-have for process-driven industries.
Supply Ability & Market Strength
Our supply ability ensures timely order completion for bulk consignments across India and global export markets such as Southeast Asia and the Middle East. Leveraging reliable transport services, your expenditure remains optimized from procurement to installation. Each machine undergoes stringent quality checks and secure packaging, reinforcing our commitment to efficient, cost-effective delivery for domestic and international clientele alike.
FAQ's of Lifting Bag Centrifuge Machine:
Q: How does the Lifting Bag Centrifuge Machine enhance industrial operations?
A: The Lifting Bag Centrifuge Machine streamlines solid-liquid separation, providing brilliant efficiency and minimizing manual labor. Its powerful lifting bag system enables fast, safe loading/unloading, while robust safety interlocks protect operators during operation.Q: What industries benefit most from this centrifuge machine?
A: Industries such as pharmaceutical, chemical, food processing, textiles, dyestuff manufacturing, and environmental sectors derive top-ranking advantages from its high separation efficiency and GMP/cGMP compliance.Q: Where can this machine be installed?
A: The centrifuge can be floor-mounted in any standard industrial facility with minimal foundation requirements, thanks to its heavy-duty construction and versatile design. It fits well in laboratories, production areas, or process plants.Q: What is the process for ordering and installing this machine?
A: Once you place your order, we manage all requirements from customization to transport services and installation. Optional on-site installation support ensures seamless setup, reducing overall expenditure and operational delays.Q: How do users benefit from the safety and control systems provided?
A: Brilliant safety interlocks and precise PLC/manual control systems safeguard operators and ensure reliable, low-noise operation. Digital readout options further enhance operational convenience and process tracking for end users.
Tell us about your requirement

Price:
Quantity
Select Unit
- 50
- 100
- 200
- 250
- 500
- 1000+
Additional detail
Mobile number
Email

More Products in Industrial Centrifuge Machine Category
Centrifuged Basket
Price 60000.00 INR / Unit
Minimum Order Quantity : 1 Unit
Power Source : Other, Electric
Product Type : Other, Centrifuged Basket
Color : Silver
Usage & Applications : Industrial filtration, separation of solids from liquids

ETP Centrifuge Machine
Price 60000.00 INR / Unit
Minimum Order Quantity : 1 Unit
Power Source : Other, Electric
Product Type : Other, Centrifuge Machine
Color : Grey
Usage & Applications : Effluent Treatment Plant, Chemical, Pharmaceutical, Textile, Industrial Filtration

36 TL Centrifuge Machine
Price 240000 INR / Unit
Minimum Order Quantity : 1 Unit
Power Source : Other, Electric
Product Type : Other
Color : Metallic with Blue
Usage & Applications : Industrial

WTP Basket Centrifuge Machine
Price 60000.00 INR / Unit
Minimum Order Quantity : 1 Unit
Power Source : Other, Electric
Product Type : Other, Industrial Centrifuge Machine
Color : Silver/Grey
Usage & Applications : SolidLiquid Separation, Chemical, Pharmaceutical, Dye, Textile, Food Processing

Contact Details
MARUTI ENGINEERS
GST : 24BWRPP8639L1ZJ
- Plot No. 201, Shankar Estate, Revabhai Estate Road, Amraiwadi,Ahmedabad - 380026, Gujarat, India
- Phone :08045813591

 Send Inquiry

Developed and Managed by Infocom Network Private Limited.
